10 Tips for Choosing Automated Injection Molding Machines?
Choosing an injection molding machine is no longer only a question of clamp force, shot size, or purchase price. Automated Injection Molding now connects servo drives, robotics, sensors, and production software into one manufacturing system. The decision affects cycle stability, labor exposure, scrap rates, energy consumption, and delivery performance.
Industry data shows why this decision deserves careful attention. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023, confirming continued investment in factory automation. Meanwhile, market research from Grand View Research identifies rising demand for energy-efficient and automated injection molding equipment through the decade. These figures support the trend, but they do not choose a machine for your plant. Real performance depends on material behavior, mold design, operator skills, and maintenance discipline.
Look closely at the production floor. A machine may promise a three-second cycle, yet cooling water may fluctuate, the mold may require manual trimming, or a robot may pause between cycles. Small delays become expensive over thousands of shots. Faster is not always better. A stable process often wins.
This guide presents ten practical tips for evaluating automated injection molding machines. It considers machine architecture, control systems, robotics compatibility, energy use, safety features, data access, service support, and total operating cost. Some recommendations may seem obvious. They are still frequently missed. A reliable choice combines supplier evidence, trial results, and honest review of your factory’s limitations. That last part is uncomfortable, but necessary.
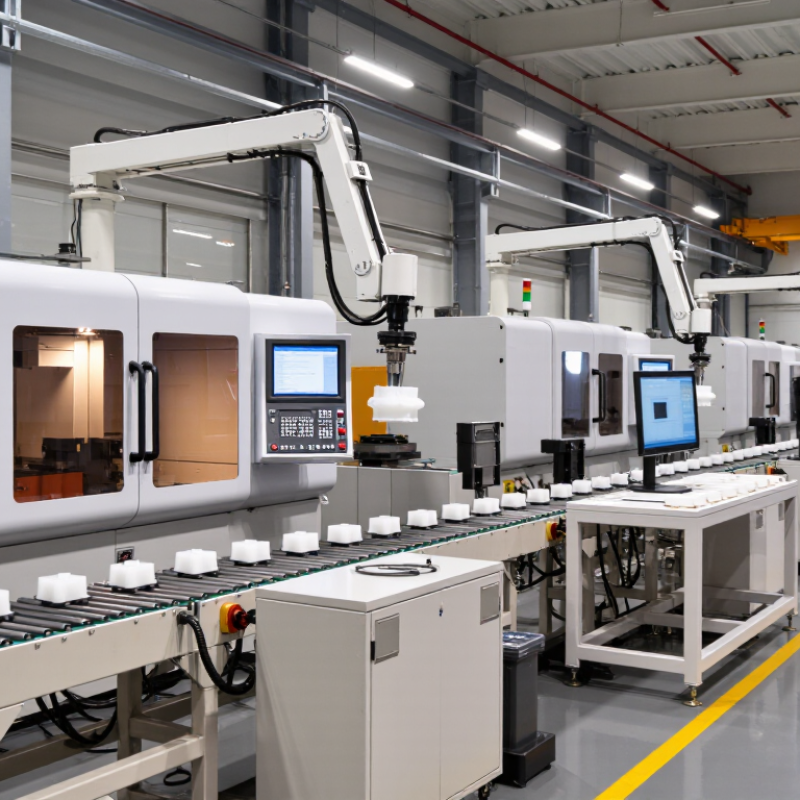
Table of Contents [Hide]
Define Part, Material, and Tonnage Needs with a 1–5% Clamp-Force Margin
Choosing an automated injection molding machine starts with the part, not the control panel. Measure projected area, wall thickness, part weight, and runner size. Include every cavity and the cold or hot runner system. A small runner can change the calculation significantly. Record the resin grade, glass content, melt temperature, and expected shrinkage. These details affect flow resistance and cavity pressure.
Calculate clamp-force needs from projected area and expected cavity pressure. When the process data are reliable, add a controlled 1–5% clamp-force margin. For an 80-ton requirement, that means roughly 80.8 to 84 tons. Select the next practical machine size, rather than forcing a borderline fit. The margin should protect against normal variation, not hide poor calculations. Thin walls, long flow paths, and uneven filling may require deeper analysis. More force is not automatically better. Excessive force can increase flash risk, mold stress, and energy use.
I have seen early estimates fail because the runner area was forgotten. That mistake was expensive. Use mold-flow results, previous production records, or a controlled trial when available. Check clamp-force readings, cavity pressure, and parting-line flash during testing. Review the data after several cycles, not just one successful shot. Automated monitoring helps, but sensors can drift and operators can misread trends. Keep a written record of assumptions, material changes, and rejected parts. The calculation may still be imperfect. That is why validation matters.
10 Tips for Choosing Automated Injection Molding Machines? - Define Part, Material, and Tonnage Needs with a 1–5% Clamp-Force Margin
| Tip | Decision Area | Data to Define | Practical Check or Benchmark | Selection Action | Priority |
|---|---|---|---|---|---|
| 1 | Part envelope | Length, width, height, wall thickness, undercuts, inserts, and ejection direction. | Record the maximum molded-part envelope and the required mold-opening direction. Thin walls and long flow paths generally increase filling difficulty. | Confirm mold daylight, tie-bar spacing, platen dimensions, mold thickness range, and ejector stroke before comparing machine models. | Critical |
| 2 | Projected area | Projected area of all cavities plus runners, measured on the parting plane. | Clamp-force estimates are commonly based on projected area multiplied by a material- and geometry-dependent cavity-pressure factor. | Use the actual projected area from the mold design or CAD data; do not size the machine from part weight alone. | Critical |
| 3 | Clamp-force margin | Calculated clamp force and selected nominal machine capacity. | Recommended selection: calculated requirement × 1.01 to 1.05. The 1–5% margin is a sizing buffer, not a substitute for mold-flow validation. | Choose the next available clamp-force class above the calculated value while avoiding excessive force that may increase mold stress and flash risk. | Critical |
| 4 | Resin selection | Resin type, grade, melt-flow rate, glass or mineral content, shrinkage, drying requirements, and processing temperature. | Engineering and fiber-filled materials can require higher processing temperatures, greater wear resistance, or different venting and drying practices than general-purpose resins. | Match barrel temperature range, screw design, check ring, corrosion or abrasion resistance, and dryer capacity to the resin datasheet. | High |
| 5 | Shot size | Total shot weight: parts plus runners, including expected process variation. | A practical target is to keep the normal shot within approximately 20–80% of the machine's rated shot capacity; confirm the supplier's stated basis and resin density. | Select injection capacity that supports the required shot without routinely operating at the extreme ends of the barrel capacity. | High |
| 6 | Injection performance | Required fill time, injection speed, peak injection pressure, and pressure-holding profile. | Thin-wall, long-flow, or high-viscosity applications may need higher injection speed and pressure than short, thick-wall parts. | Compare available injection rate and pressure at the intended screw position, not only the machine's headline maximum. | High |
| 7 | Cycle time | Cooling time, mold-open time, ejection time, injection time, and expected cycles per hour. | Cooling is often the largest portion of the cycle for thermoplastic parts; actual time depends on wall thickness, resin, mold temperature, and cooling-channel design. | Evaluate platen motion, acceleration, dry-cycle time, controller repeatability, and the machine's ability to sustain the target cycle. | Medium |
| 8 | Automation interface | Robot signals, mold-protection logic, part-present confirmation, conveyor interface, safety circuits, and recipe exchange. | Automated cells require coordinated handshakes for mold open, robot entry, part removal, mold close, and fault recovery. | Request the input/output list, communication protocol, safety-category documentation, and recovery sequence before installation. | High |
| 9 | Quality monitoring | Cushion, transfer position, injection pressure, filling time, mold-protection force, and alarm limits. | Stable process variables support repeatability, but acceptance limits should be established from validated production data rather than generic values. | Choose a controller that records trends, protects recipes, provides user access levels, and exports production data for traceability. | Medium |
| 10 | Utilities and total cost | Electrical load, cooling-water flow, compressed-air demand, floor space, maintenance access, and expected utilization. | Installed utility capacity must cover the machine, mold-temperature control, dryer, robot, and auxiliary equipment operating together. | Compare energy consumption per cycle or per kilogram, preventive-maintenance requirements, spare-parts availability, training, and commissioning support. | Medium |
Clamp-force planning note: Calculate the required force from the projected mold area and the expected cavity-pressure condition for the selected resin, part geometry, and process. Apply a 1–5% selection margin, then verify the result through mold-flow analysis, trial molding, and flash inspection. Final machine selection should also satisfy mold dimensions, shot capacity, injection performance, automation requirements, and applicable safety regulations.